1. Smartly improve basic security features
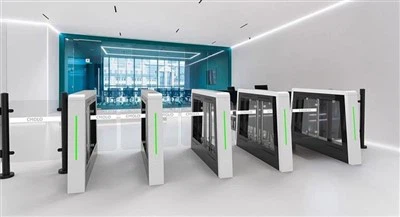
The main benefit of turnstiles is that they safeguard people in two ways: by keeping them physically apart and by recognizing them intelligently. The full-height rotary gate can rotate 120° or 90°, and it automatically locks when each person passes through, which keeps traffic behind it from getting through. For example, the SA101 cross dual channel full height turnstile used in a certain chain supermarket can use its 15° anti-reverse technology to keep an eye on the direction of rotation in real time. The brake lever locks the brakes in 0.3 seconds when a reverse intrusion is detected. The sound and light alarm system raises the success percentage of stopping people from going through the wrong way to 99.6%.
The turnstile builds a three-dimensional protective net out of several multi-level sensor arrays to stop people from tailgating. One smart gate system uses a combination of infrared radiation and millimeter wave radar to precisely determine the following behavior within a range of 0.5 meters. When an abnormal route is found, it not only sets off a local alarm, but it also connects to the video surveillance system so that the target may be instantly tracked. The data shows that the method has cut down on supermarket entrance thefts by 72%.
The optimized design of mechanical structures makes safety even better. The equipment can work safely in temperatures between -20 and 60 degrees Celsius, thanks to a fully stainless steel rainproof shell and a hydraulic shock absorber movement. It has an IP45 protection level. A certain supermarket's turnstile has a feature that automatically resets it. It locks or closes automatically after 10 seconds if there is no passage, which stops the risk of channel congestion.
2. Function growth and experience optimization based on scenarios
The value of turnstiles is shown by how well they solve problems in supermarket operations. The equipment can work with an EAS electronic anti-theft system to help keep losses to a minimum. The gate will automatically lock and sound an alarm if someone tries to get through with products that haven't been paid for. A particular supermarket connected the turnstile to the RFID tag system. This cut the number of items that were missed by scans from 3.2% to 0.8% and saved the store over 2 million yuan in losses per year.
The new use of the passenger flow management function is changing how supermarkets work. A certain smart supermarket has a turnstile system with a counting module. This module can count things like how many customers enter the store and how long they remain in real time. Using the POS system for association analysis, it was discovered that the busiest time for customers is from 3 to 5 p.m. on weekends, however the conversion rate is lower than on weekdays. Because of this, changing the promotion strategy led to an 18% rise in sales during this time.
When it comes to dealing with unusual situations, turnstiles are very adaptable. As a result of the outbreak, a store has added an infrared temperature sensor module to its turnstile. It immediately stops and sends a notice to the management staff when it detects an abnormal body temperature. With a false warning rate of less than 0.1%, the system can handle more than 20,000 passenger flows every day, which helps keep people safe and prevents the spread of disease.
3. Support for operational decisions based on data
The huge amount of traffic data that turnstiles collect is becoming a significant tool for running supermarkets more efficiently. A specific chain supermarket looked at their gate data and found that 45% of the people who came in every Tuesday morning between 10 and 11 am were older. Because of this, they did more to promote fresh food at this time, which led to a 25% rise in sales for this category. This specific marketing based on customer profiles boosts the return on investment of marketing resources by three times.
Using an equipment failure warning system cuts down on the costs of running and maintaining the system by a large amount. The sensor in the turnstile at a given supermarket can keep an eye on things like movement temperature and motor current in real time. If it finds something wrong, it will automatically make a work order. The average duration between equipment failures went from 1200 hours to 3500 hours after the system was put in place, and the cost of maintenance was down by 40% per year.
The fire linkage function of turnstiles is very important for managing emergencies. When a fire broke out in a supermarket, the turnstile opened on its own within two seconds of getting the fire signal. The emergency lighting system let people leave the store 60% faster. The idea of "combining peacetime and wartime" in this design lets equipment be very useful in both normal and emergency situations.
Tripod Turnstile Speedgate


WhatsApp : 0086-15999546575
Skype : cmolo.joy
Email : contact@cmolo.com
Tel : 0086-15999546575
CMOLO Industrial Park,NO. 144-1, Hengping Road,Henggang Street, Longgang District, Shenzhen City, China